Engineering & manufacturing

From design development to production process

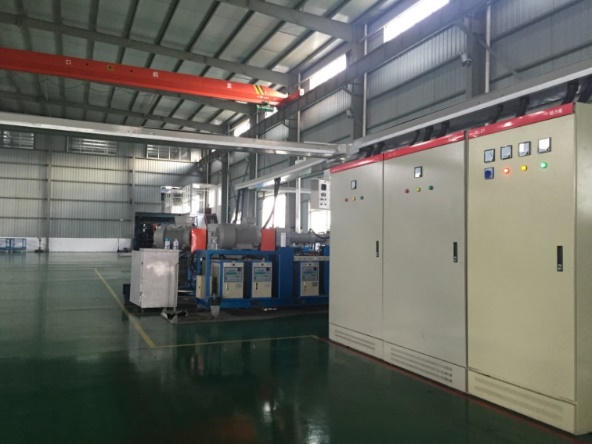
The technical centre handles design and tooling development; production runs on automatic batching, co-extrusion and finishing equipment; the laboratory covers material, performance and environmental testing.

Capability map

Design, tooling, manufacturing, testing

Design & development

Design & development

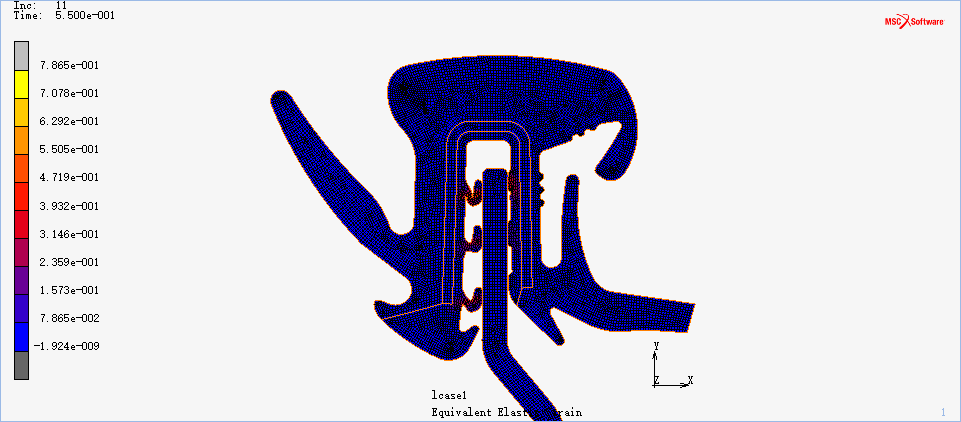
Design capability across EPDM, PVC and TPE sealing profiles, with simultaneous engineering and drawing-based development. 3D design in CATIA / UG, CAE analysis for insertion/extraction force and sealing performance, projects managed through the five APQP phases.
Tooling & manufacturing

Tooling & manufacturing

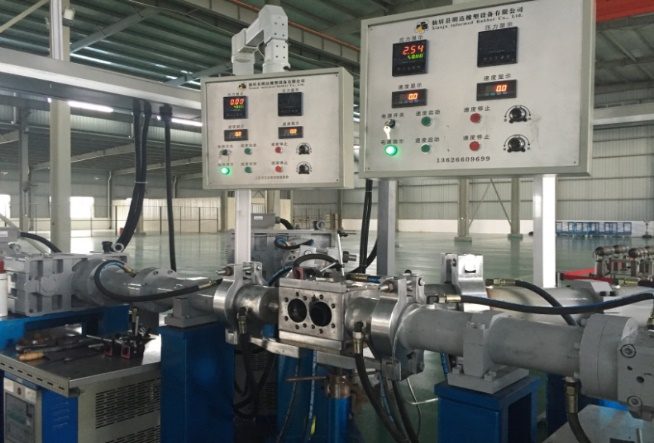
Tooling is designed in-house, machined by wire EDM and maintained by dedicated fitters. Production runs on automatic batching, five rubber and one plastic co-extrusion lines, covering steel-carrier roll forming, hard-soft co-extrusion, flocking, coating, punching and tape application.

Test laboratory

Test laboratory

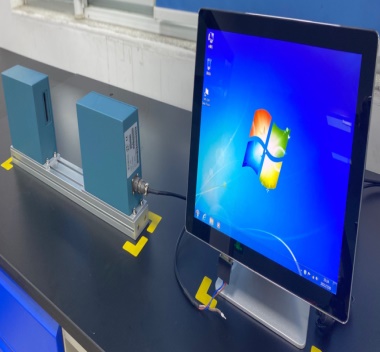
Material, performance and environmental test equipment - rheometer, Mooney viscometer, tensile and abrasion testers, laser gauge, damp-heat, ozone, UV, xenon and salt-fog chambers - supporting sample validation and production monitoring.

Design tools

Simultaneous engineering and CAE

3D design in CATIA V5 and UG NX, 2D in AutoCAD; CAE in Marc Mentat for insertion / extraction force on body seals and sealing performance on small and panoramic sunroof seals.

3DCATIA V5 · UG NX

3D section and tooling design; data exchange for simultaneous engineering

2DAutoCAD

2D drawings and fixture drawings

CAEMarc Mentat

Insertion/extraction force, compression load and sealing simulation

PMAPQP

Concept → approval → sample qualification → pre-production → launch

Production

Thirteen steps from batching to tape application

Batching → mixing → milling → co-extrusion → heat setting and vulcanisation → cooling → plasma treatment → coating → curing → inspection → cutting → molded corners → tape application.

Co-extrusion line
Key equipment
  • Automatic minor / major ingredient weighing with barcode material tracking
  • Five rubber and one plastic co-extrusion lines with closed-loop process control
  • Steel-carrier forming, electrostatic flocking, ovens and vulcanisation zone
  • Automatic end-shape punching dies and multi-hole punching press
  • Automatic PSA / hot-melt tape applicators, film and paste splicers, PE-film cold splicer
  • Semi- and fully-automatic rubber injection presses
Request equipment and capacity data
Project flow

From brief to launch

01Brief

Application, section, material, volume and timing

02Design & review

3D design, CAE analysis, tooling and process plan

03Sample approval

Samples, test reports and vehicle-level validation

04Pre-launch & SOP

PPAP, process control, traceability and improvement